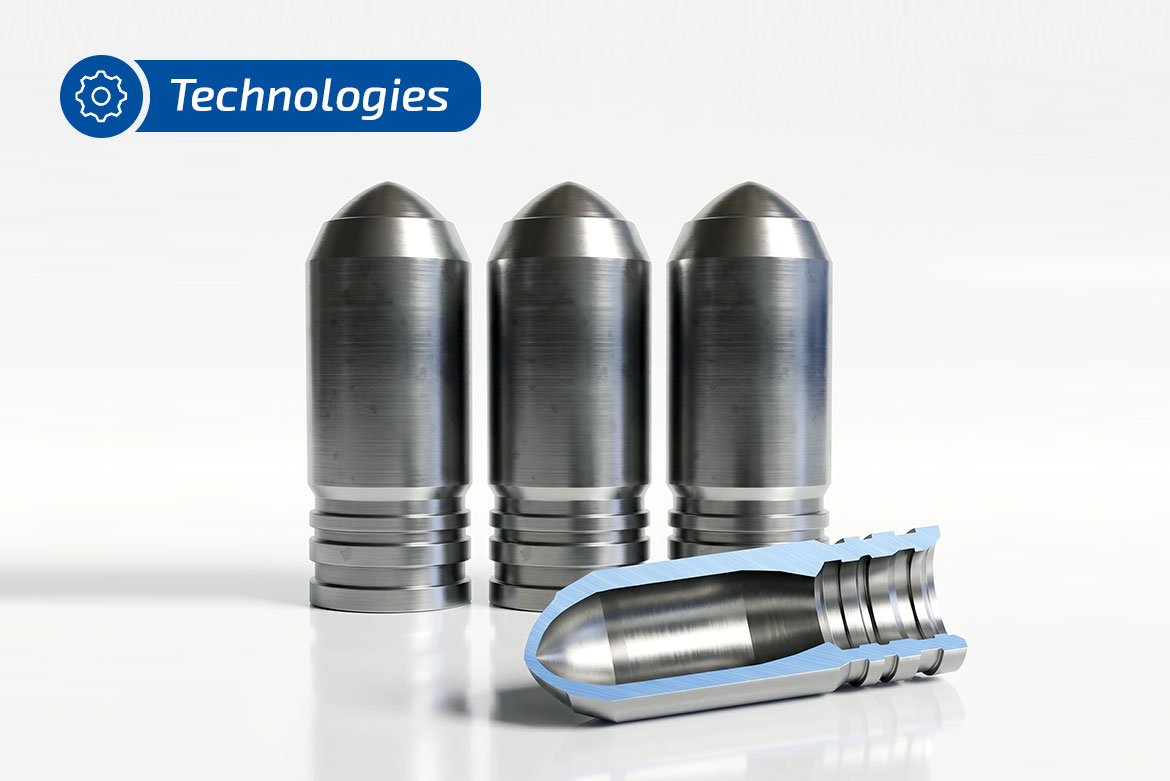
EMAG has developed a production line concept for 120mm tank ammunition built around the VL 8 vertical pick-up turning machine. The projectile body is machined from solid stock in three operations, starting with drilling and internal turning, moving to external machining, and finishing with threads and undercuts. This article describes the workpiece, the machine, the process sequence, line design, and automation, and the results of the machining tests.
Oliver Hagenlocher
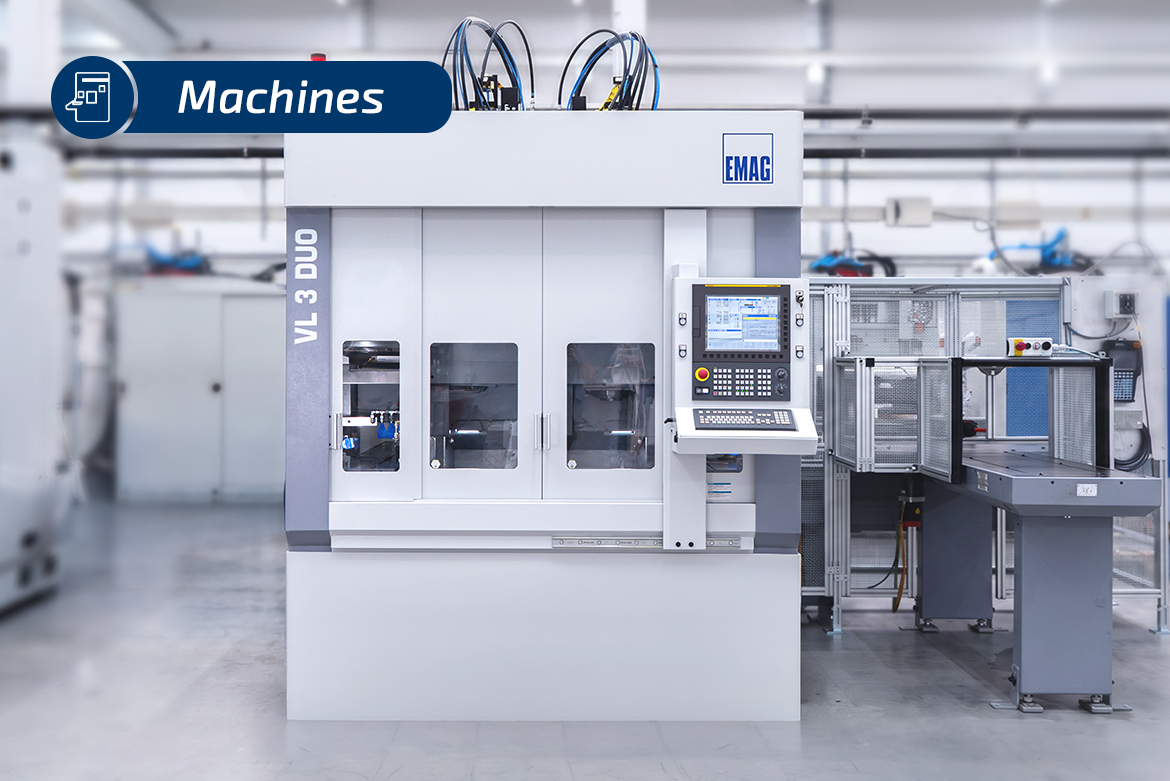
Skilled labor shortages, cost pressures, and limited floor space are challenges every manufacturer faces. For high-volume production of chucked components, that means getting more parts out of every shift and every square meter. This is where EMAG’s VL 3 DUO comes in. The dual-spindle turning machine combines two work spindles and integrates pick-up automation with TrackMotion and a parts magazine in just 24.5 m². This article highlights the benefits this offers.
Scroll free turning is a turning process developed by EMAG in which a straight cutting edge, set at a 45-degree angle, sweeps tangentially past the rotating workpiece. The point of contact continuously moves along the cutting edge. This produces twist-free surfaces with grinding-quality finishes – significantly faster than with conventional finish-machining and completely dry.
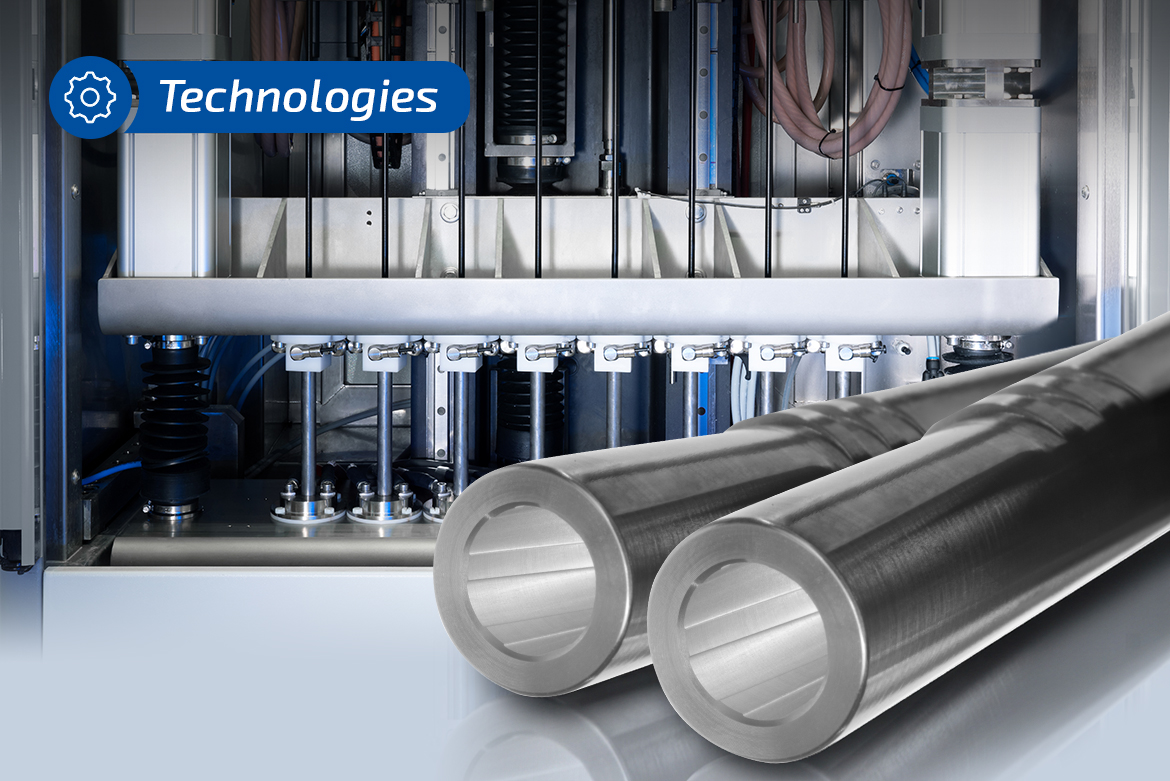
Weapon barrel manufacturing ranks among the most demanding challenges in long-part machining. Extreme length-to-diameter ratios, tight concentricity tolerances, hard-to-machine materials, and the unique internal geometry with rifling and lands present unique challenges at every process step. This article describes the complete process chain from the sawn raw-part to the barrel ready for installation. Comparing a hammered tube to one machined with ECM highlights the machining and process requirements needed for reliable production. This example doesn’t cover other rifling methods, like button rifling or cut rifling.
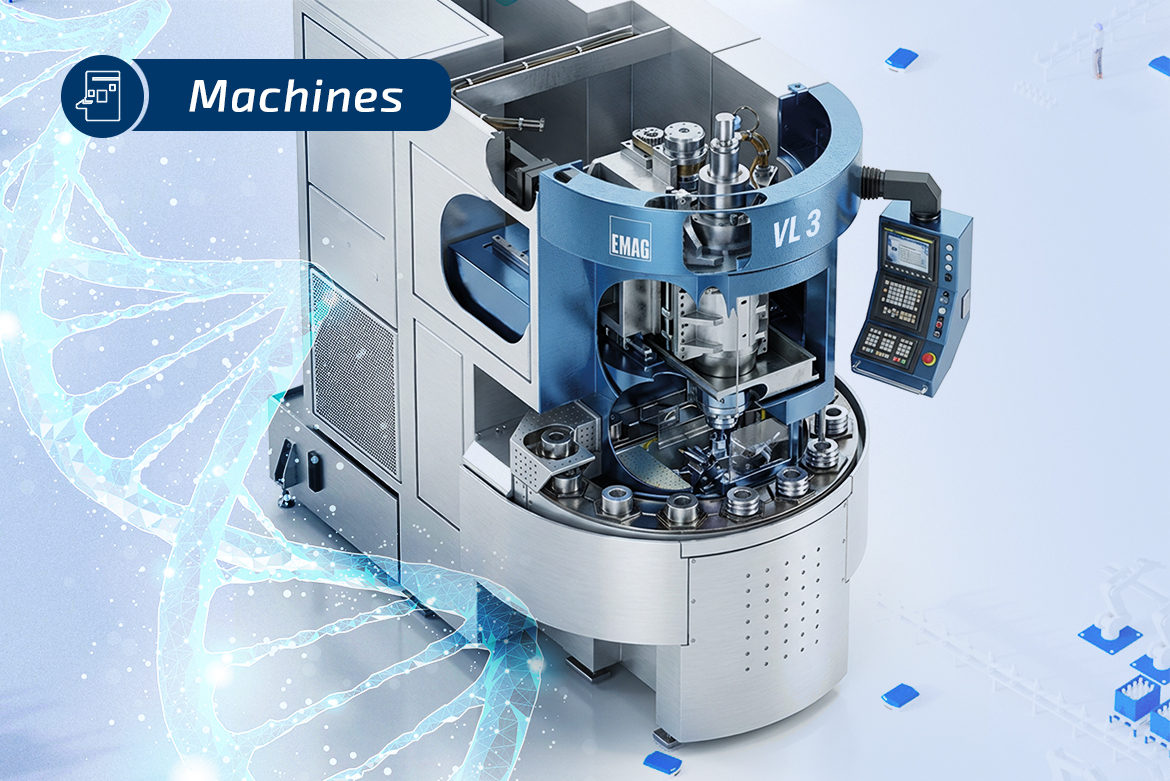
A rebuild mechanically restores a proven VL machine to reliable production-ready condition. Instead of accepting declining precision, increasing downtime risks, or diminishing performance, the machine undergoes a targeted overhaul. For operators of the VL 3, VL 5, and VL 5i, this provides a predictable alternative to purchasing new equipment.
In batch production in particular, it’s not just machine availability that counts. What matters most is that the system produces with consistent precision, maintains stable cycle times, and avoids unplanned downtime. With a professional rebuild, key mechanical assemblies are replaced or overhauled, restoring the machine to original precision and continued to use productively.
In small chucked component production, demands for precision and cost-effectiveness are on the rise. Gear wheels, planetary gears, sprockets, cam rings, pump rings, individual cams, or shaft generators must be precisely finished after hardening. Tight dimensional and geometric tolerances, stable positional relationships, and defined surface qualities are required for high-volume production.
The VL 100 GT from EMAG is designed for this task. The vertical turning and grinding center combines hard turning and grinding in a single machine and enables high-precision finishing of small chucked components up to 100 millimeters in diameter in a single setup. This reduces reclamping errors, shortens process times, and achieves the required surface quality.
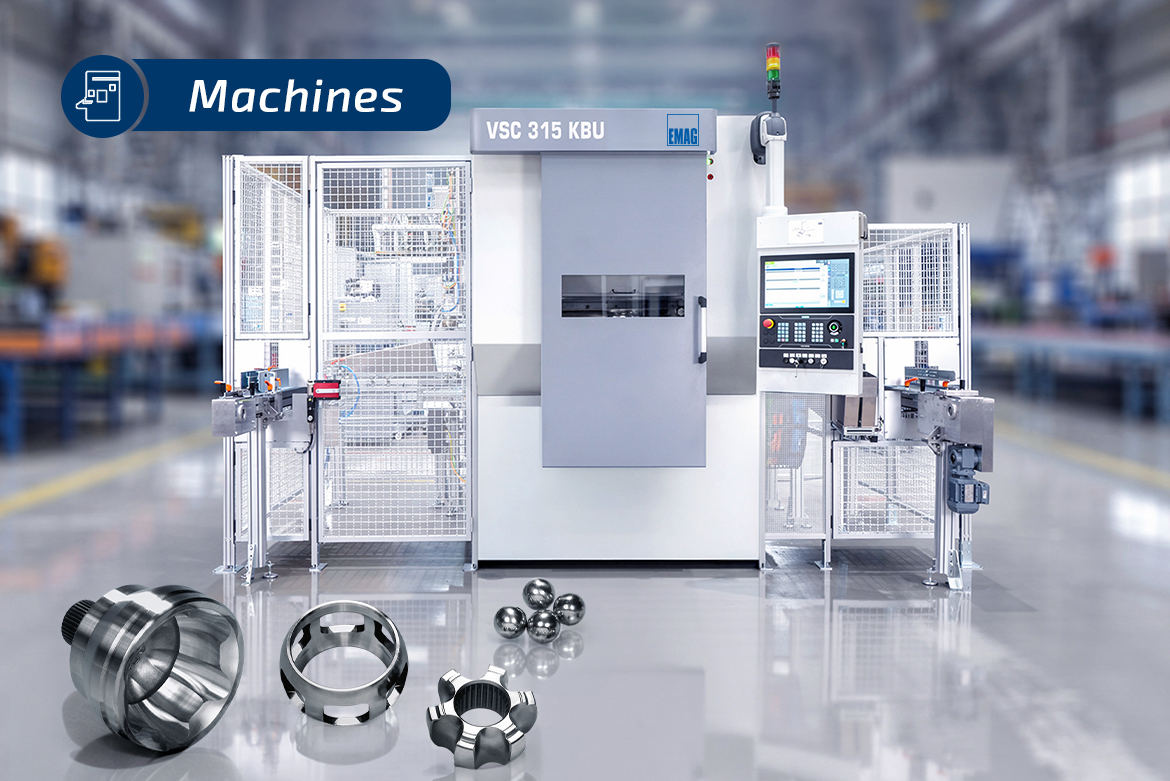
Joint housings are among the most technically demanding components in automotive drivetrains. Together with inner races, ball cages, and outer races, they form the basis for CV joints, which enable uniform power transmission between two axles—even with varying angles and length compensation. The manufacturing quality of the ball tracks in these components directly determines the functionality, smoothness, and service life of the entire drivetrain.
With the rise of electric mobility, the focus in manufacturing is shifting significantly: Components that could “run along” in internal combustion engines due to masking noises and vibrations are evaluated much more critically in electric drives. The reason is simple: The internal combustion engine generates a broad spectrum of noise that masks many background sounds. In electric drives, this acoustic “background noise” is largely absent, making deviations in shape, position, and surface significantly more noticeable.
The production of steering pinions poses a particular challenge in the modern automotive industry. These precision gear components are indispensable parts of steering systems and must meet the highest quality standards while also being produced economically in large quantities. The combination of required dimensional accuracy, surface finish, and process stability demands specialized manufacturing solutions.
In this interview, Konstantin Ungefuk, Head of the Gear Cutting Soft Business Unit at EMAG, explains the complex process chain involved in machining steering pinions. He provides detailed insights into every machining step – from turning the raw-parts to soft-state gear hobbing, precision grinding of the bearing seats after hardening, and the final skiving of the hardened tooth profiles.
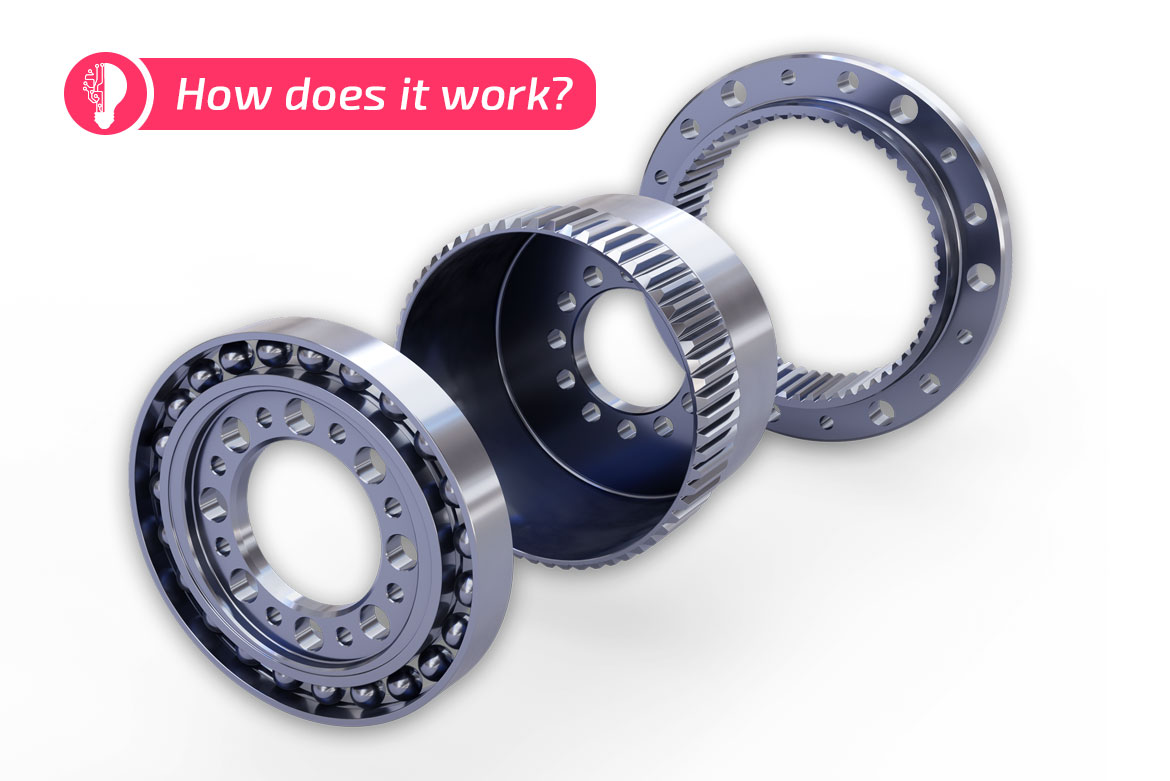
Strain wave gearboxes are an indispensable part of precision drive systems. They play a central role in robotics, automation technology, and positioning axes with high accuracy requirements in particular. But what exactly is the operating principle behind this gear technology, and why is it particularly suitable for compact, low-backlash drive solutions?