Grinding, Hard turning, or Scroll free turning? There are three methods to choose from for the precision machining of seal and bearing seats, and each has its ideal application. This comparison highlights the differences in surface quality, cycle time, and cost, and explains which criteria are decisive when selecting a method.
Whether it’s a rotor shaft, a gear shaft, or an outer race: At the end of the manufacturing process, finishing determines the component’s function and service life. For seal and bearing seats, there are essentially three methods to choose from: grinding, hard turning, and Scroll free turning. Which one is worthwhile depends on the required surface finish, the machining length, the quantity, and the process costs. This article compares the three methods.
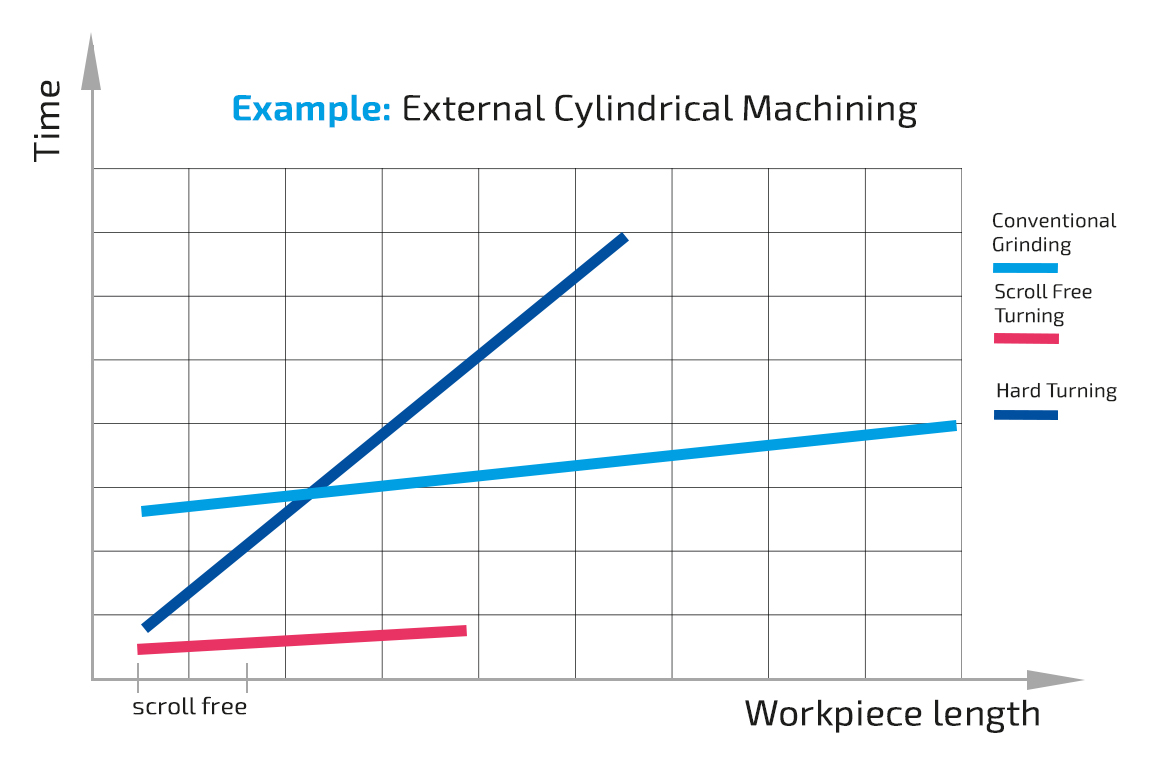
Processing time versus processing length: With hard turning, the time increases sharply; with grinding, it remains flat at a high level. Scroll free turning is significantly lower.
An overview of the three processes
Grinding is the traditional method for achieving the highest surface finishes. It uses an undefined cutting edge and reliably produces twist-free surfaces. Hard turning machines hardened components with a defined cutting edge directly on the lathe. It offers flexibility for contours and grooving, but – due to the nature of the process – leaves a fine feed mark on the surface, known as “twist.”
Scroll free turning bridges the gap between these two approaches. In this turning process developed by EMAG, a straight cutting edge set at a 45-degree angle sweeps tangentially past the rotating workpiece. The point of contact continuously moves along the cutting edge. This produces twist-free surfaces with grinding-quality finishes – even at feed rates more typical of rough machining. Our in-depth article “How Scroll Free Turning Works” explains the process in detail.
Surface quality: Who achieves what?
In grinding, Rz values around 1 micrometer and a finish free of tool marks are the standard. Every alternative is measured against this exact benchmark. In hard turning, the feed rate determines the surface finish: To achieve Rz 4, you must run slowly – in the example calculation, at just 0.11 millimeters per revolution. The process is free of tool marks when performed with conventional longitudinal turning, because the feed groove acts like a screw conveyor for the oil at tight fits.
In scroll free turning, the surface finish of the cutting insert is transferred to the workpiece almost one-to-one, largely irrespective of the feed rate. With two insert variants, the process covers both relevant application areas: The variant for seal seats produces Rz values of 1 to 4 (actual values 2.6 to 2.9), because the radial shaft seal requires an oil cushion and thus a defined residual roughness. The ultra-fine-ground variant achieves Rz values between 0.5 and 0.9, for applications such as bearing seats. Depending on the insert, the helical depth ranges from 0.1 to 0.8 micrometers. This places Scroll free turning on par with grinding in terms of quality.
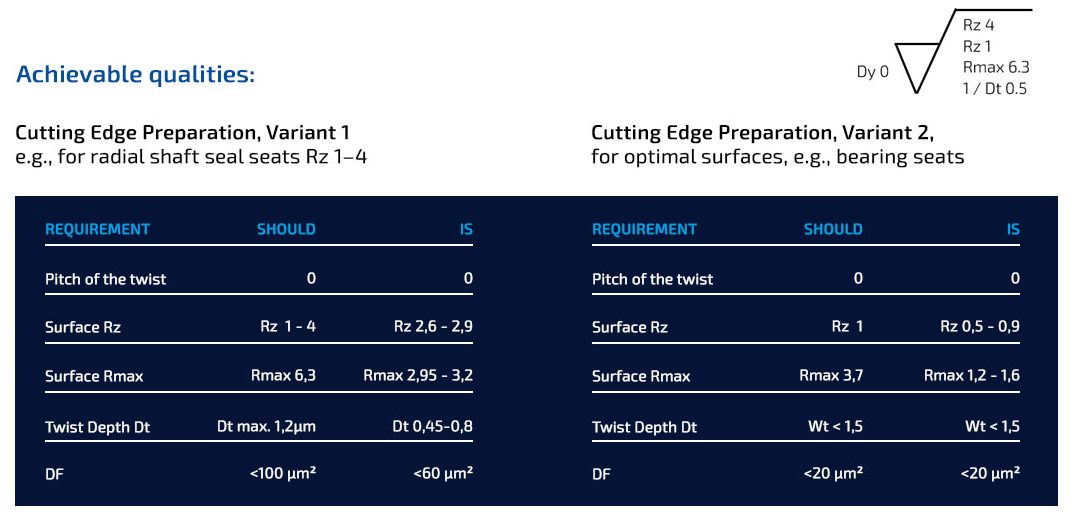
Achievable surface finishes in scroll free turning: Using two types of cutting inserts, surface finishes ranging from Rz 1 to 4 can be achieved for sealing seats, or Rz below 1 for bearing seats – all free of twist.
Cycle time and machining length: The crucial difference
If you plot machining time against machining length, the typical pattern becomes apparent: In hard turning, the time increases steeply with length due to the low feed rate. Grinding starts at a high baseline but remains comparatively flat over the length. Scroll free turning lies significantly below both curves as long as the machining length matches the cutting edge: The cutting edges are up to about 50 millimeters long; with no twist, seats up to about 35 millimeters can be machined. Longer diameters are possible with a superimposed Z-axis movement, though typically free of tool marks.
Two practical examples: In the hard machining of a bearing seat (diameter 40 millimeters, length 30 millimeters), conventional finish-machining takes 12.9 seconds. The combination of conventional pre-turning and Scroll free turning takes 10.2 seconds – a savings of 2.7 seconds per seat.
The difference is even more pronounced in the soft machining of the rotor stack: Here, the machining time drops from 22.7 to 6.1 seconds because Scroll free turning performs the finish-machining operation at a feed rate of one millimeter per revolution.
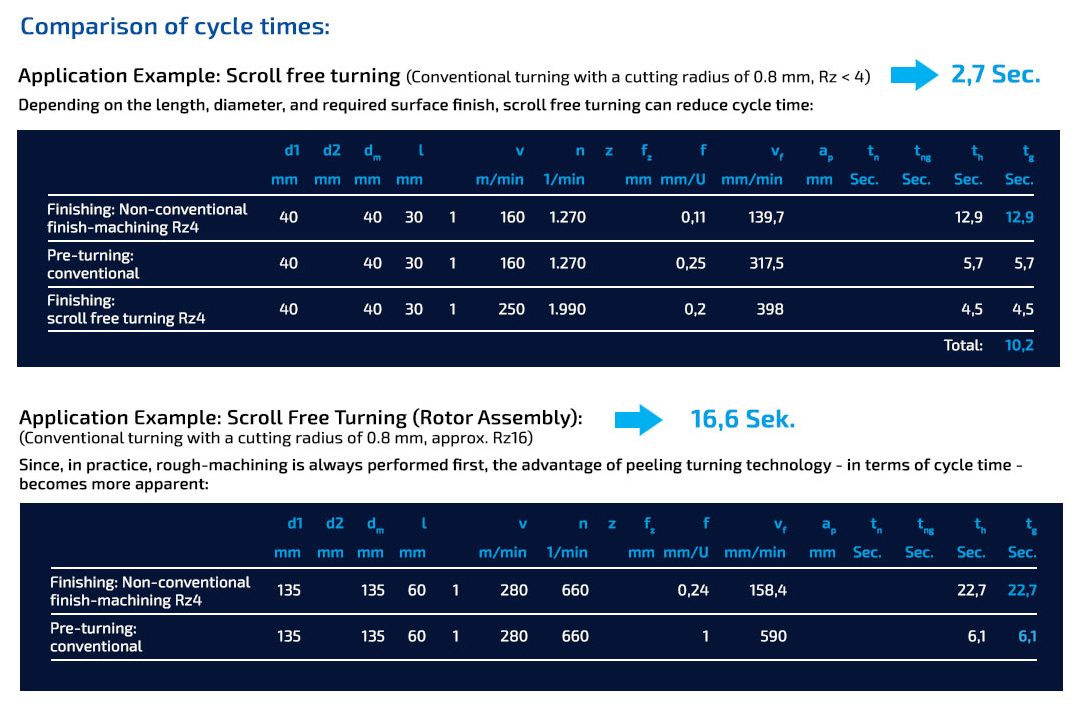
Real-world cycle time comparison: In hard machining, Scroll free turning saves 2.7 seconds per seat. For soft rotor assemblies, the machining time drops from 22.7 to 6.1 seconds.
Tool costs, tool life, and non-cutting times
In hard turning, wear limits cost-effectiveness: With a service life of about 20 minutes per cutting edge, an indexable insert produces approximately 150 workpieces in the calculation example. The peeling turning edge achieves 3,000 cuts based on a conservative estimate; in practice, tool life ranges between 2,000 and 12,000 components, depending on the material, cutting speed, and tool life criteria. For 3,000 workpieces, this means approximately 20 tool changes in hard turning compared to a single change in Scroll free turning. At two minutes per change, this saves 38 minutes of non-productive time, which translates to 1.3 seconds per workpiece.
Compared to grinding, scroll free turning offers several significant advantages in terms of process costs: It operates entirely dry, eliminating the need for cutting fluids, treatment, and disposal. Dressing cycles are also eliminated. Energy consumption and capital investments are significantly lower compared to conventional methods. The peeling tool is equipped with a special turning holder, whereas grinding requires a separate station in a combination machine or a dedicated grinding machine.
Limitations: Where each process has its limits
Scroll free turning is designed for cylindrical O/Ds. I/Ds and end faces cannot be machined. The process requires a lathe with a Y-axis and a stable workpiece clamping system, as the radial forces are higher than in conventional turning. In addition, the initial quality of the workpiece plays a role: In practice, conventional turning is usually performed first to compensate for runout errors.
Hard machining on the outer race: After conventional pre-turning, the finishing cut with the peeling tool produces a twist-free surface, completely dry.
Grinding remains the first choice for internal machining, end faces, and very long, twist-free seats, as well as wherever process chains and approvals are designed for grinding. Hard turning retains its strengths for contours, grooves, and complex geometries. Often, the answer isn’t an either/or question anyway: On EMAG machines, the processes can be combined – for example, turning and grinding, or conventional pre-turning and Scroll free turning – in a single setup on the VT series.
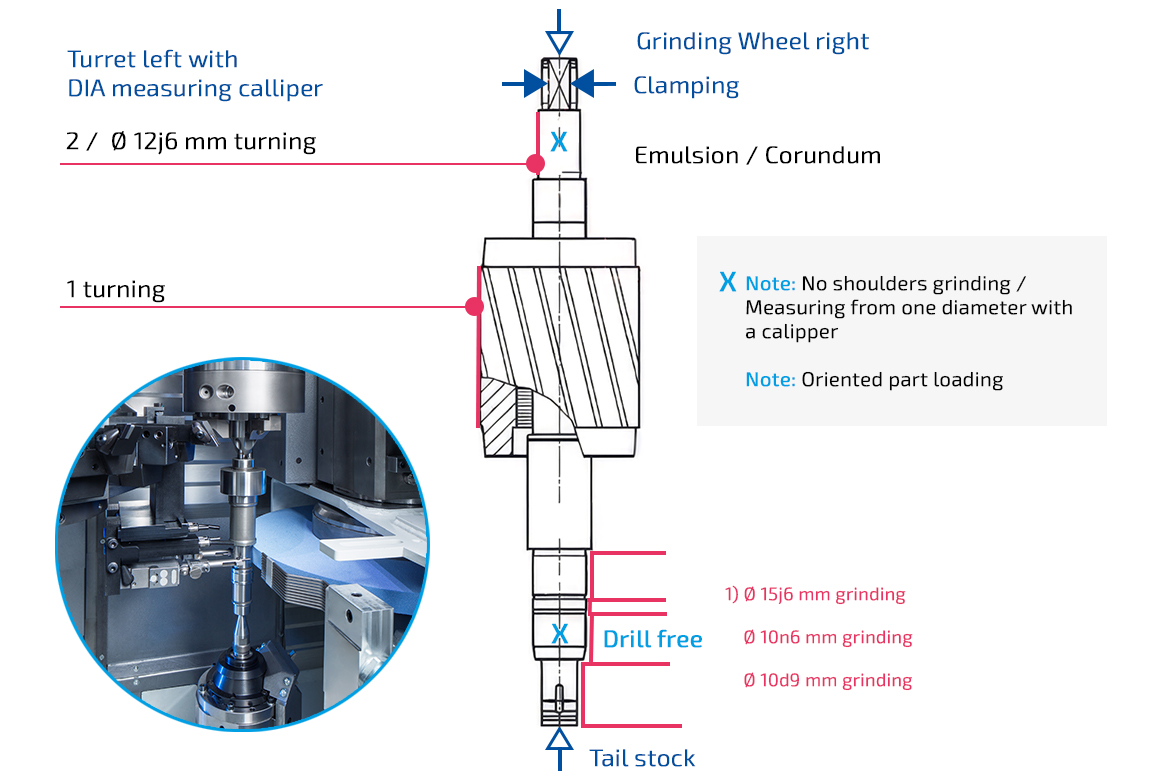
When grinding is specified: The process plan for the VT 100 GT combines turning and grinding in a single setup, for example, for bearing seats with grinding specifications.
Practical decision-making guide
As a rule of thumb for selecting a process: For non-twist sealing and bearing seats on cylindrical O/Ds – especially for high-volume production – scroll free turning is usually the fastest and most cost-effective solution. For contours, recesses, and complex geometries, hard turning remains the standard choice, often combined with Scroll free turning for the seats. For I/D (Inner Diameter), end faces , and very long twist-free machining operations, grinding remains the preferred method.
A process design based on our own component demonstrates the potential cost savings in a specific case. Our article “Rotor Shafts for Electric Drives” (Rotor shafts in electric drives: Types & interfaces) provides deeper insight into the requirements of e-mobility, while the article on the VL 100 GT vertical turning and grinding center illustrates the combination of turning and grinding.