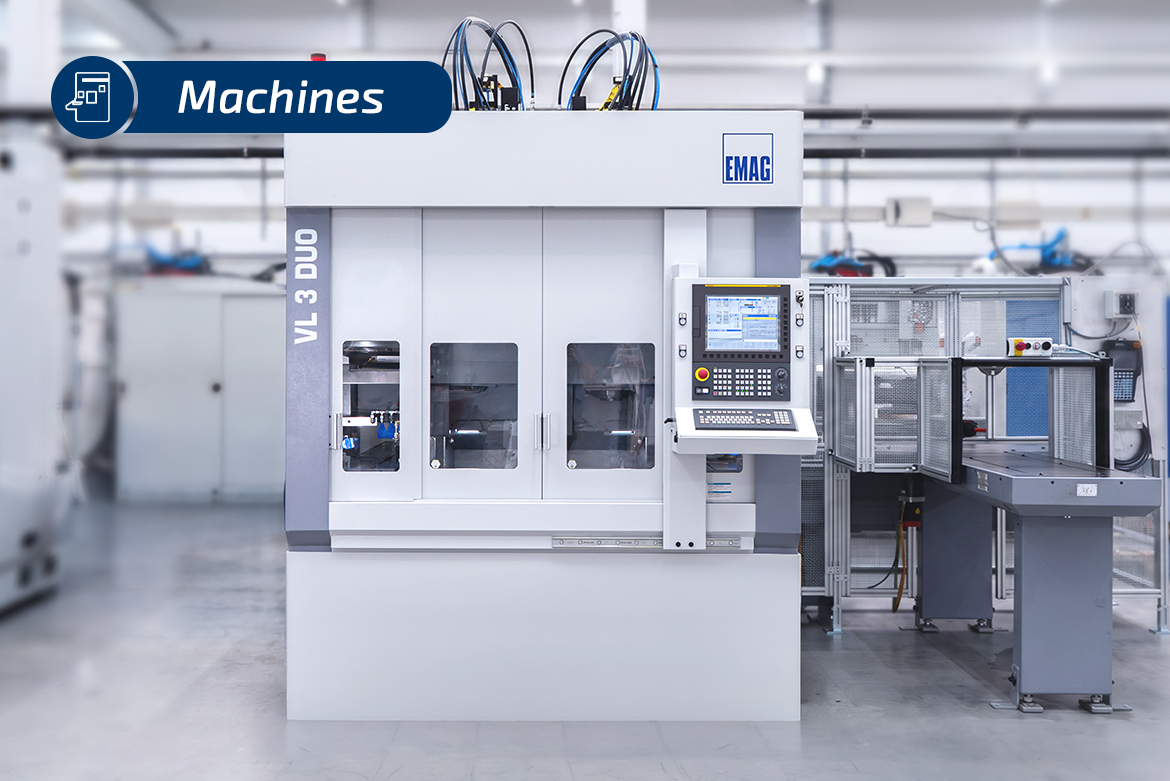
Skilled labor shortages, cost pressures, and limited floor space are challenges every manufacturer faces. For high-volume production of chucked components, that means getting more parts out of every shift and every square meter. This is where EMAG’s VL 3 DUO comes in. The dual-spindle turning machine combines two work spindles and integrates pick-up automation with TrackMotion and a parts magazine in just 24.5 m². This article highlights the benefits this offers.Â
Machines
A rebuild mechanically restores a proven VL machine to reliable production-ready condition. Instead of accepting declining precision, increasing downtime risks, or diminishing performance, the machine undergoes a targeted overhaul. For operators of the VL 3, VL 5, and VL 5i, this provides a predictable alternative to purchasing new equipment.Â
In batch production in particular, it’s not just machine availability that counts. What matters most is that the system produces with consistent precision, maintains stable cycle times, and avoids unplanned downtime. With a professional rebuild, key mechanical assemblies are replaced or overhauled, restoring the machine to original precision and continued to use productively.Â
In small chucked component production, demands for precision and cost-effectiveness are on the rise. Gear wheels, planetary gears, sprockets, cam rings, pump rings, individual cams, or shaft generators must be precisely finished after hardening. Tight dimensional and geometric tolerances, stable positional relationships, and defined surface qualities are required for high-volume production.
The VL 100 GT from EMAG is designed for this task. The vertical turning and grinding center combines hard turning and grinding in a single machine and enables high-precision finishing of small chucked components up to 100 millimeters in diameter in a single setup. This reduces reclamping errors, shortens process times, and achieves the required surface quality.
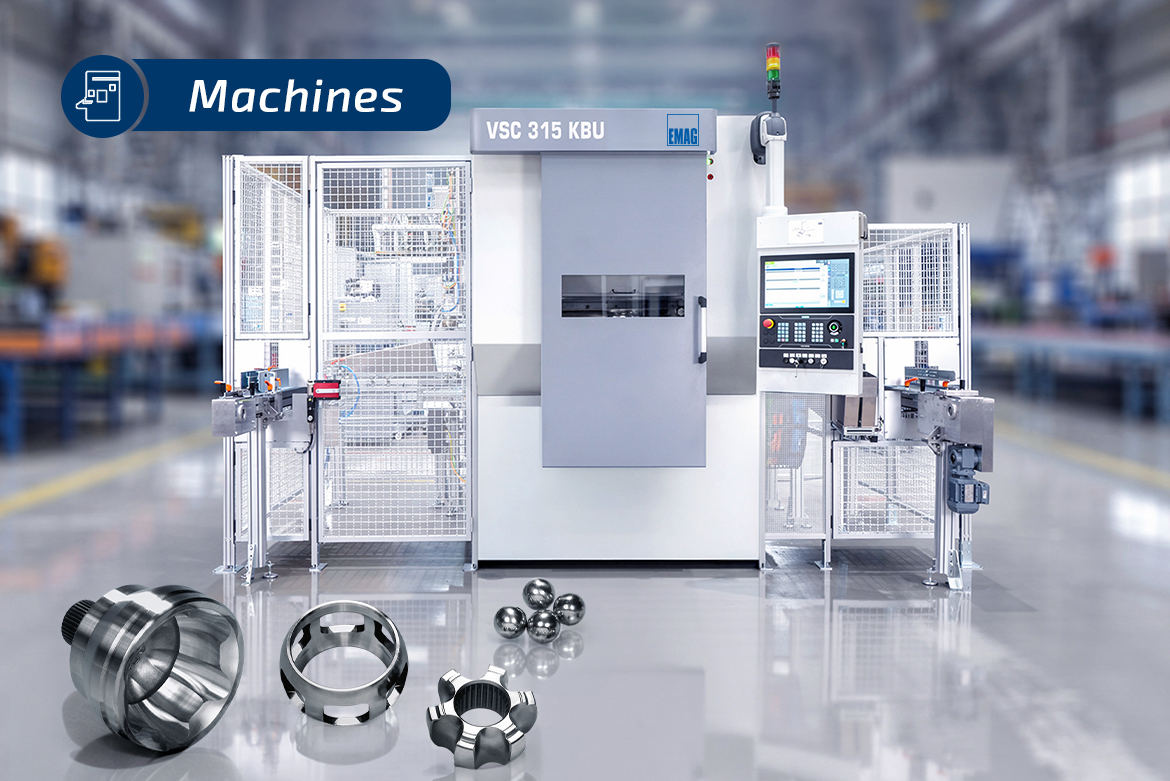
Joint housings are among the most technically demanding components in automotive drivetrains. Together with inner races, ball cages, and outer races, they form the basis for CV joints, which enable uniform power transmission between two axles—even with varying angles and length compensation. The manufacturing quality of the ball tracks in these components directly determines the functionality, smoothness, and service life of the entire drivetrain.Â
The manufacturing industry faces the challenge of using production space more efficiently while also reducing process times. When machining flange parts, such as differential housings, several separate machining stations are required in conventional production. The VT 200 with counter spindle option shows how modern turning machines can address these challenges through process integration.
The machining of thin-walled workpieces is a complex task in manufacturing technology. Hardened rings and gears in particular exhibit considerable shape deviations after heat treatment. These components typically have elliptical, potato-shaped or triangular contours instead of the required circular shape. During subsequent lathe machining, conventional clamping systems often fail to achieve the required roundness tolerances.
The central challenge lies both in the deviation of the clamping diameter and in the interaction between workholding technology and cutting forces. While traditional diaphragm chucks, collet chucks or centering and face chucks can guarantee a mechanical fixation, out-of-round workpieces inevitably deform, leaving  free arc segments between the clamping points. At these points, the lathe tool presses the thin-walled component outwards, which leads to additional shape deviations after spring-back. Even with optimized workholding technology, conventional processes often reach their limit at roundness values of 20 to 30 µm.
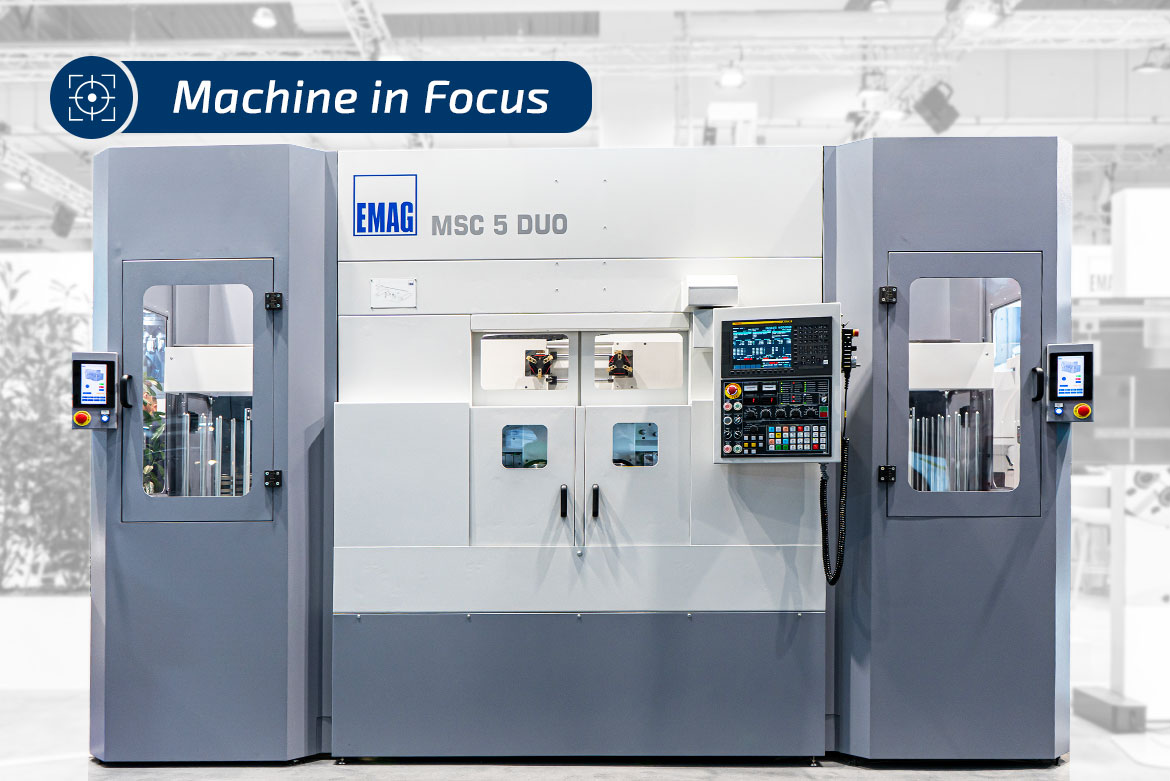
The automated production of turned parts in medium and large batch production requires CNC turning machines that combine productivity, process reliability and cost-effectiveness. The MSC 5 DUO from EMAG’s Classic series addresses these requirements with a machine configuration consistently designed for automation. As a fully automated CNC lathe with a double-spindle concept, the machine is positioned in the compact manufacturing cell segment for workpieces up to 120 mm in diameter and 85 mm in length.Â
Daniel Rujanoski is Director of Global Sales & Applications at EMAG LaserTec and is responsible for technical sales and the Laser Application Center. In this interview, the expert in laser welding technology explains the technical features and cost-saving advantages of the new ELC 6i – a standardized laser welding cell for powertrain components.Â
Stepped planetary gears are a key component in the drivetrains of electric vehicles. These components must meet high precision requirements while remaining cost-effective for series production. The combination of geometric complexity and tight tolerances demands sophisticated manufacturing concepts.
Double helical gears are a special type of gear in which two helical gears are arranged in a mirror image configuration on the same shaft. This design can withstand high loads and is significantly more cost-effective to manufacture than herringbone tooth profiles. Double helical gearing combines the advantages of helical gearing, which can absorb high loads, with the additional benefit of compensating for axial forces through its mirror-image arrangement.Â